Author: admin_flifeac

  • PT Royal Coconut Kawangkoan

    PT Royal Coconut Kawangkoan

    PT Royal Coconut Kawangkoan

    High Quality, Certified and Reliable Coconut Products PT Royal Coconut was established on April 25, 2007, initially only in the industrial processing of coconut into desiccated coconut. There are a lot of desiccated coconut materials used to mix in biscuits, chocolate, ice cream, and other snack products. The export market for desiccated coconut covers Western and Eastern European countries, and now it has spread to Turkey and even to other Middle Eastern countries.
  • PT Biomol Nusantara Mandiri

    PT Biomol Nusantara Mandiri

    PT Biomol Nusantara Mandiri

    PT Biomol Nusantara Mandiri operates in the field of health biotechnology and veterinary pharmaceuticals. The company is engaged in research and development, production, and distribution of biotechnology-based products, particularly vaccines and veterinary medicines. With integrated operations covering R&D, manufacturing, quality control, and distribution, PT Biomol Nusantara Mandiri focuses on delivering high-quality and reliable products to support animal health and the veterinary industry in Indonesia. Historically, the company originated as part of PT Tekad Mandiri Citra, a major producer, importer, and distributor of veterinary medicines based in Bandung, West Java. Building on this strong foundation, PT Biomol Nusantara Mandiri continues to develop and produce biotechnology-based veterinary products through structured research processes and controlled manufacturing standards. Through continuous innovation and expertise in veterinary health, PT Biomol Nusantara Mandiri contributes to the advancement of the vaccine and veterinary medicine sector, supporting sustainable animal health and biosecurity in Indonesia.

  • Explosion-Proof AC

    Explosion-Proof AC

    Explosion-Proof AC

    Return air type/Fresh air type

    Description

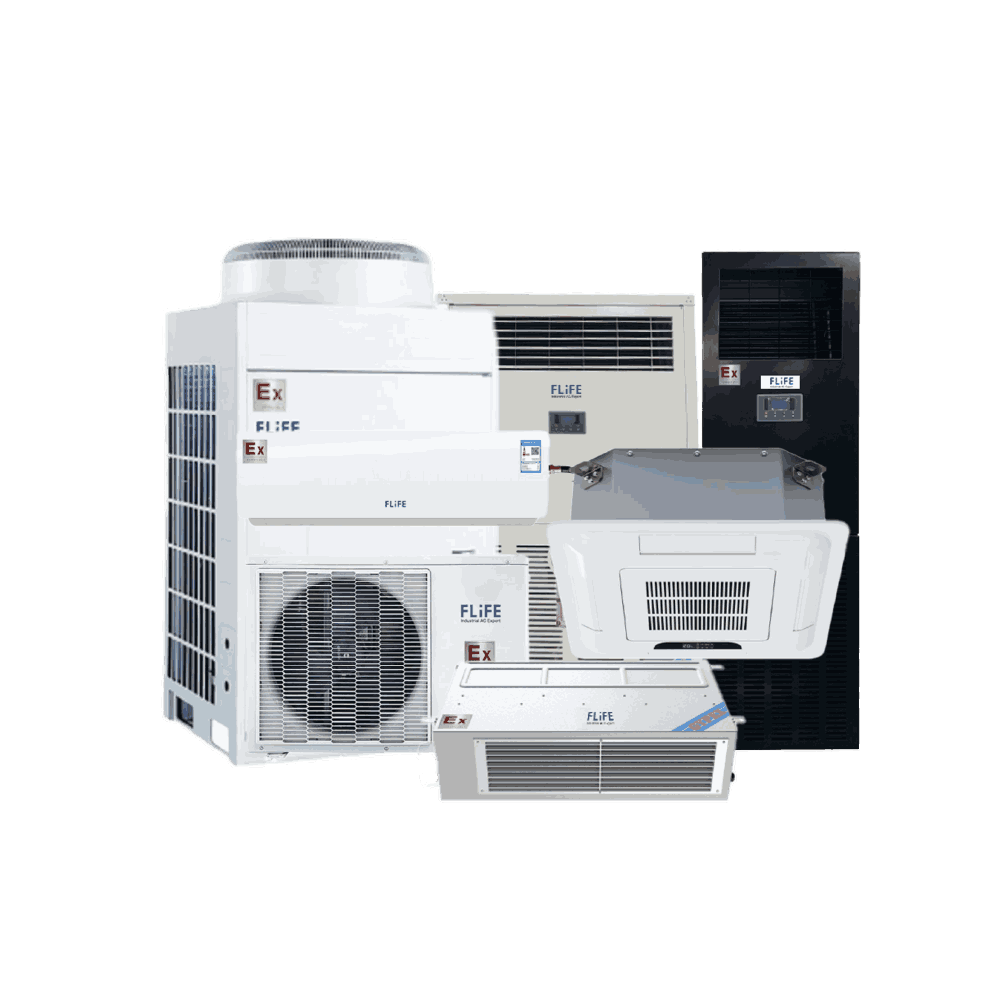
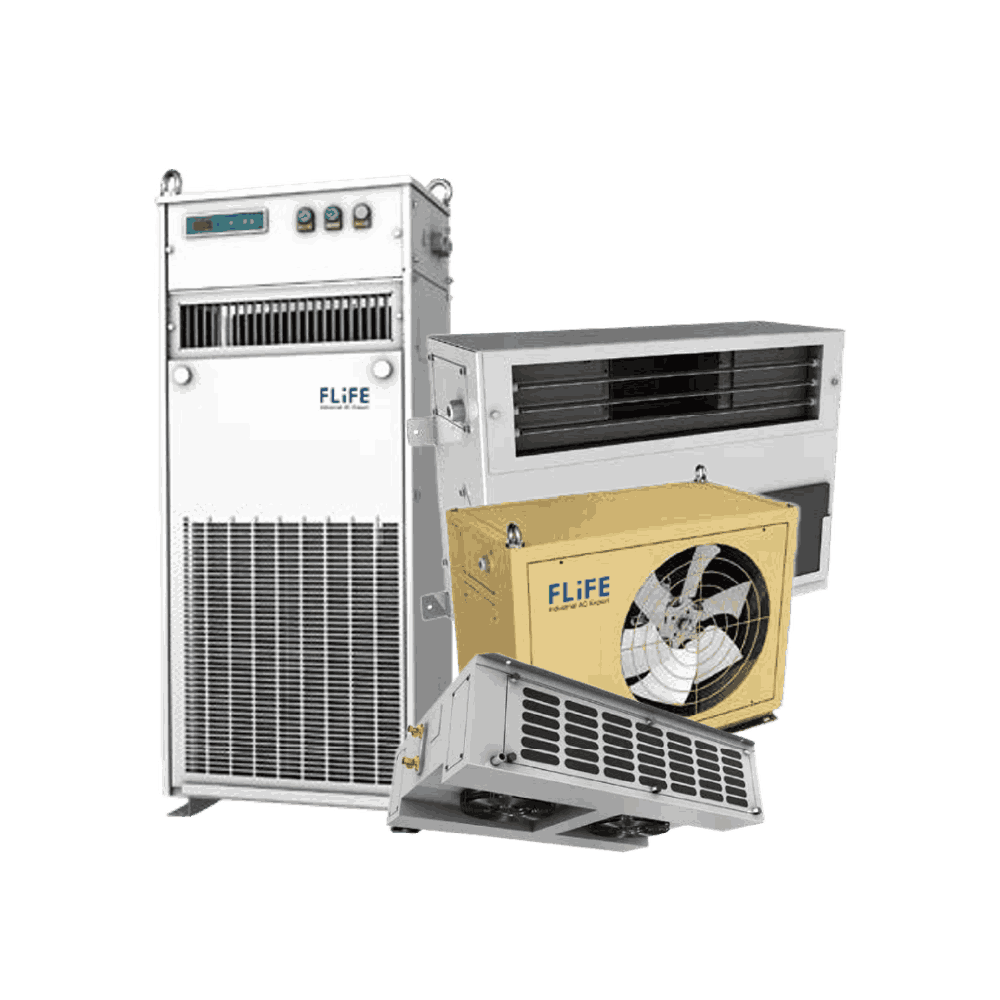
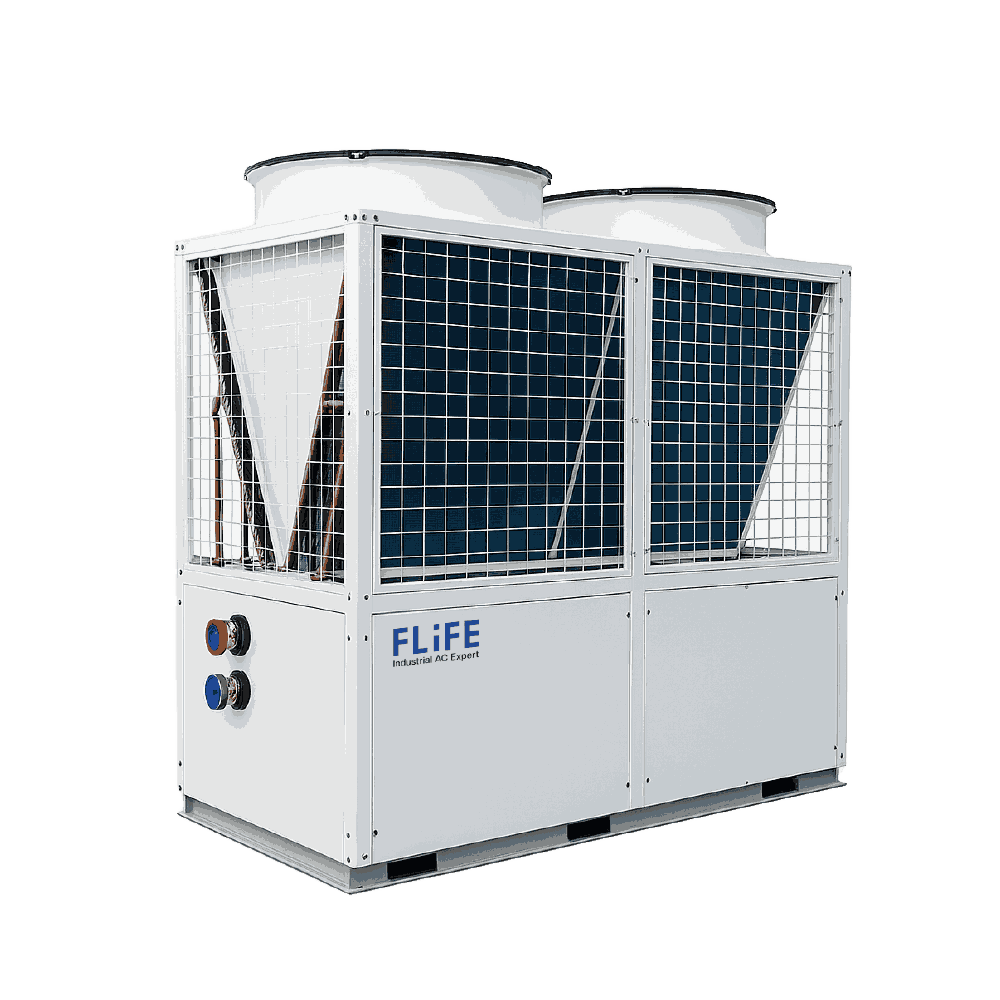
    FLIFE Explosion-proof air conditioners combine ​advanced safety mechanisms and ​intelligent controls to serve critical roles in hazardous industries.
    Core Advantages:

    1. Explosion-Proof Design and Safety
    • ​Full-Unit Protection: Critical components (compressors, fans) use composite technologies like flameproof (Exd), intrinsically safe (Exib), and encapsulated (Exm) designs to eliminate sparks
      ​- Robust Materials: Stainless steel or corrosion-resistant alloy housings ensure durability in extreme conditions
      ​- Safety Monitoring: Built-in gas concentration sensors and temperature/humidity detectors trigger automatic shutdowns or alarms for abnormalities
    1. ​Efficient Cooling/Heating and Stability
    • ​Multi-Finned Heat Exchangers: Improve refrigerant-air contact, enhancing cooling/heating efficiency by 20–30% compared to standard units
    • ​Wide Temperature Range: Operates in -15°C to +65°C environments, suitable for both high-temperature workshops and low-temperature storage
    1. ​Smart Controls and Energy Efficiency
    • ​Inverter Technology: Adjusts compressor speed to reduce energy consumption (EER ≥3.5)
    • ​Remote Management: Supports IoT-enabled monitoring via mobile apps or computers for centralized oversight

    Versatile Applications:
    ​​High-Risk Industrial Environments

    • ​Oil and Gas: Refineries, chemical plants, and fuel storage areas (Ex IIA/IIB-rated)
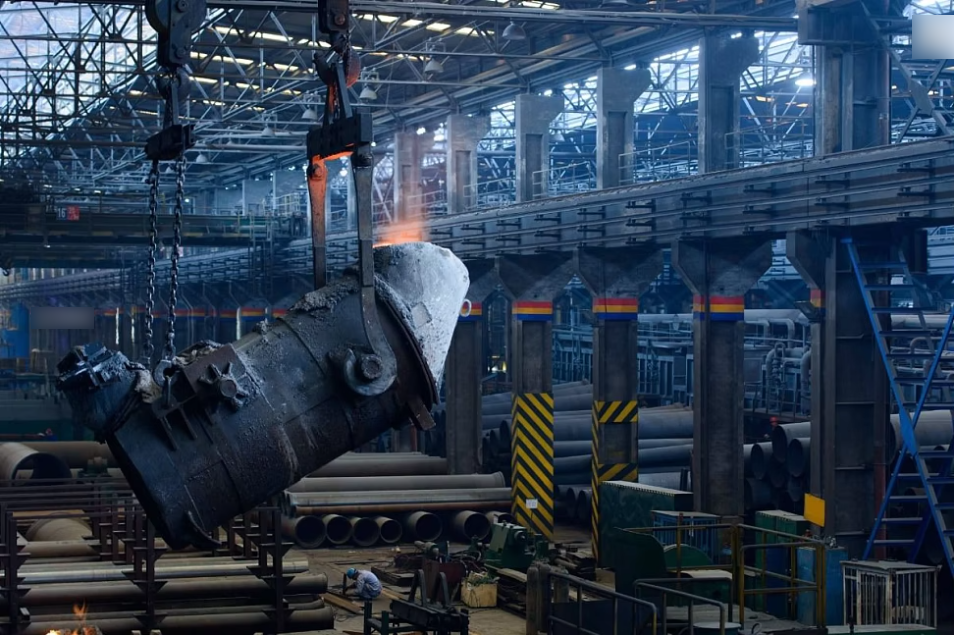
    • ​Mining and Metallurgy: Customized units for underground mines or metal smelting facilities
      ​Specialized Facilities
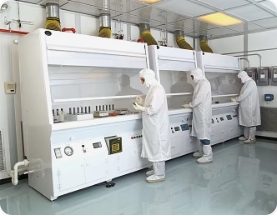
    • ​Military and Research: Ammunition depots, labs handling volatile substances
    • ​Pharmaceuticals and Food: Alcohol extraction rooms, flour processing plants (Ex IIC-rated)
      ​Extreme Environments and Mobile Scenarios
    • ​Offshore Platforms: Resists saltwater corrosion and high humidity
    • ​Modular Units: Rapid deployment in temporary mining camps or containerized control rooms
  • High-Temperature AC

    High-Temperature AC

    High-Temperature AC

    Description

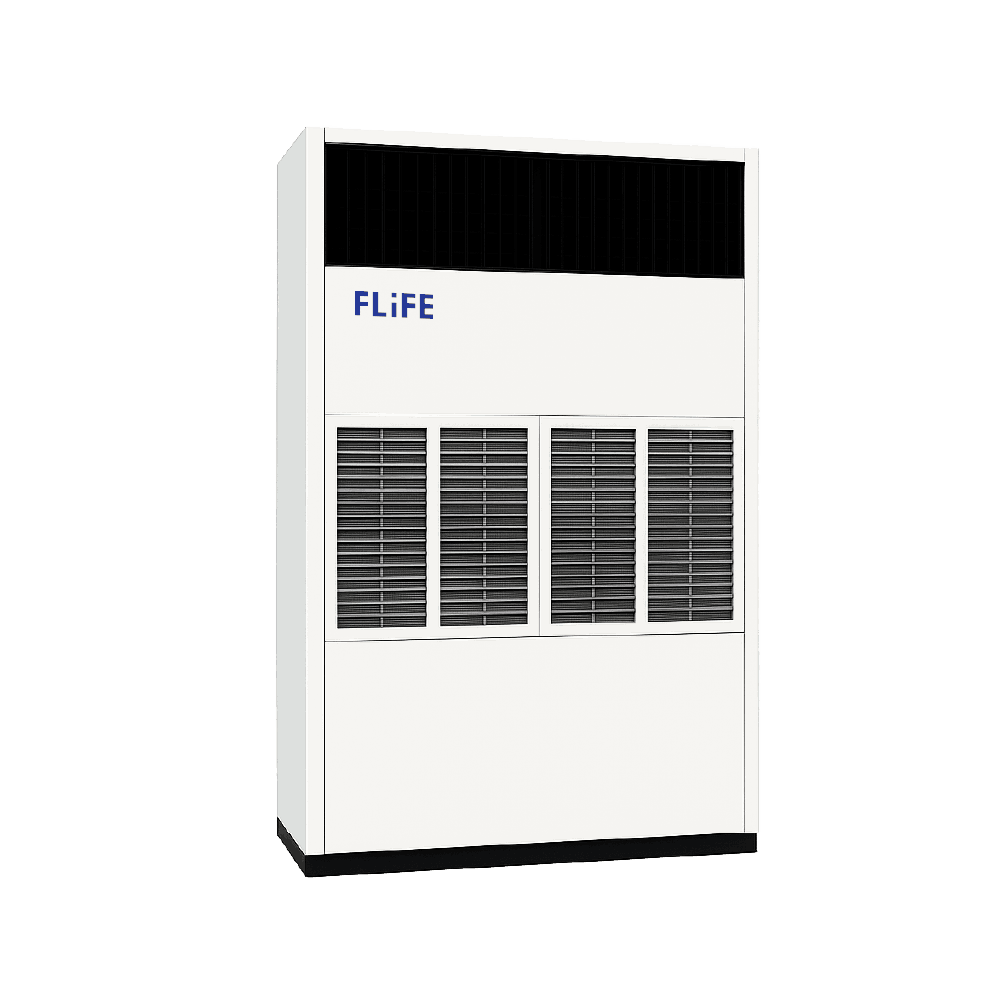
    FLIFE High-temperature air conditioners excel in ​industrial resilience, ​smart operation, and ​energy efficiency, making them indispensable for extreme environments.
    Core Advantages:

    1. Heat Resistance and Stability
    • ​High-Temperature Materials: Critical components (compressors, condensers) use heat-resistant steel, ceramics, and other durable materials to ensure stable operation in 60°C–90°C environments
      ​- Thermal Protection: Built-in sensors and automatic shutdown mechanisms prevent overheating
    1. ​Efficient Cooling and Rapid Temperature Control
    • ​Advanced Refrigerants: Optimized refrigerants (e.g., eco-friendly options) and enhanced circulation systems improve heat transfer, achieving 20–30% faster cooling than standard units
    • ​Wide Operating Range: Functions in -15°C to 65°C, suitable for both freezing warehouses and high-temperature workshops
    1. ​Smart Control and Remote Management
    • ​Precision Temperature Control: Real-time adjustments via sensors maintain temperature accuracy within ±0.5°C
      ​- Remote Monitoring: Manage settings via mobile apps or computers for centralized oversight
    1. ​Energy Efficiency and Sustainability
    • ​Inverter Technology: Adjusts compressor speed based on load, reducing energy consumption (EER ≥3.5)
    • ​Eco-Friendly Refrigerants: Low-GWP (Global Warming Potential) refrigerants comply with environmental regulations
    1. ​Durability and Environmental Resilience
    • ​Corrosion Resistance: Stainless steel or galvanized shells withstand dust and chemical exposure (e.g., hydrogen fluoride in chemical plants)
    • ​Anti-Vibration Design: Dual-inlet centrifugal fans and shock-resistant brackets suit mining and metallurgy applications
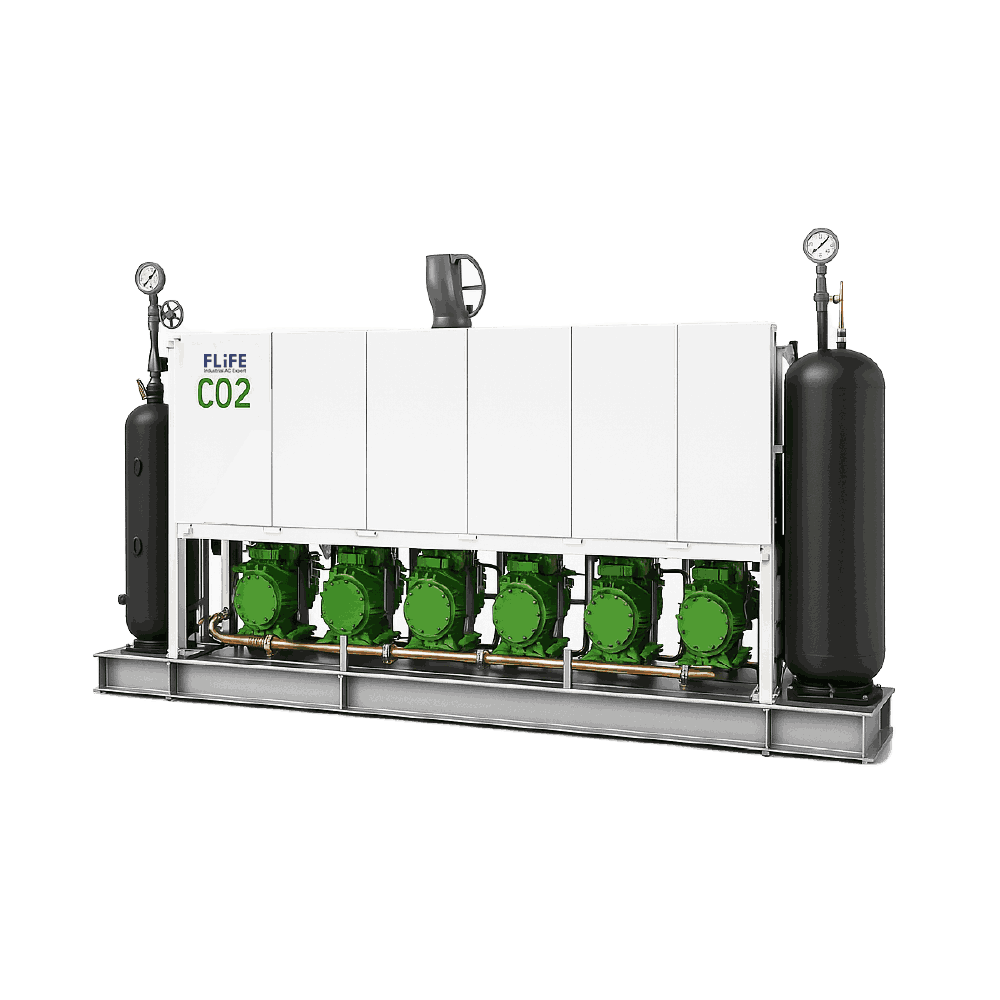
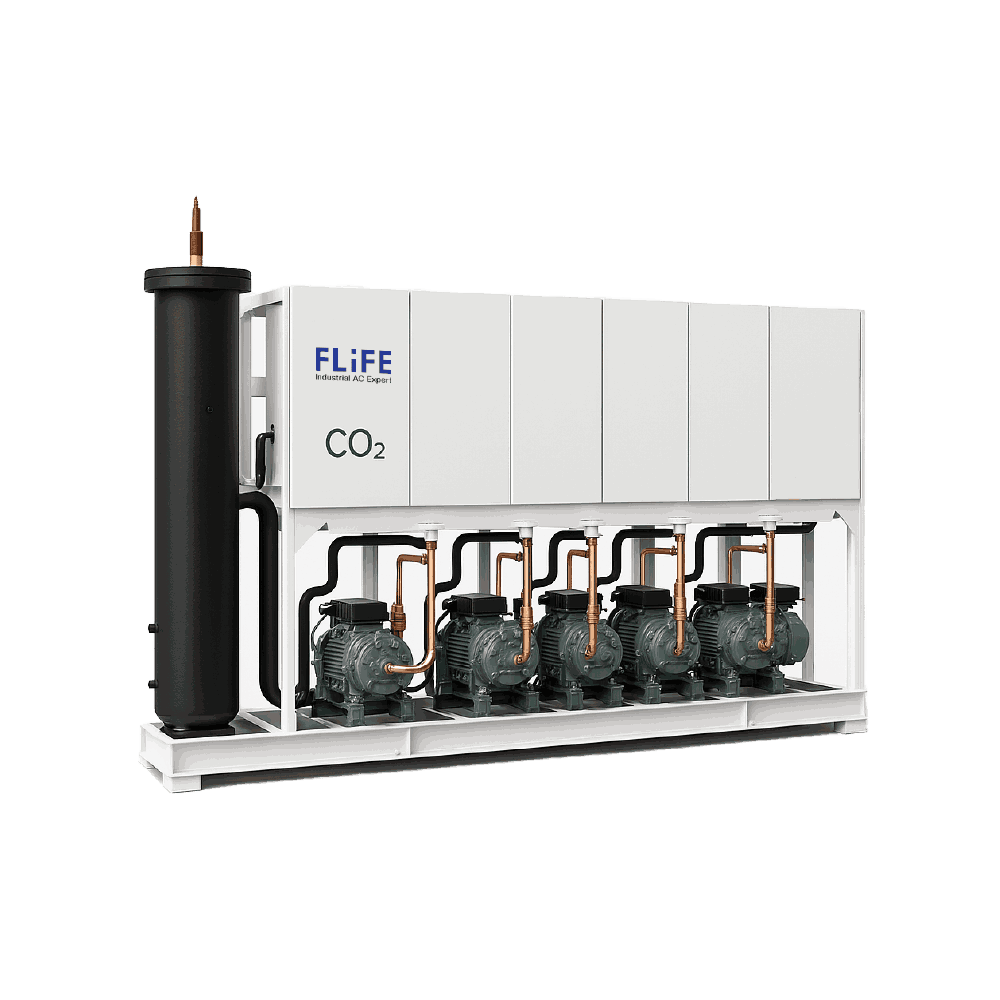
  • Cold Chain System

    Cold Chain System

    Cold Chain System

    Return air type/Fresh air type

    Description

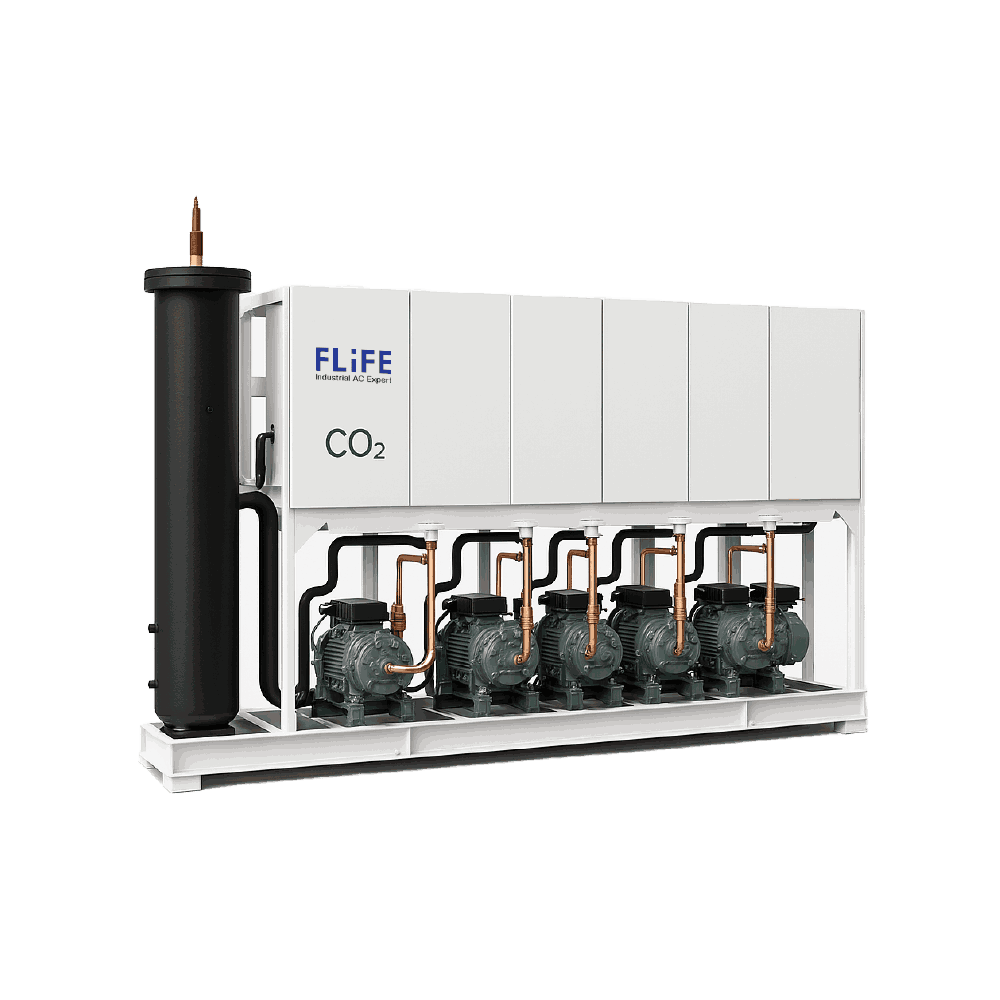
    Selection Guidelines:

    1. Capacity Matching:
      Small (<500 tons) for retail, large (>10,000 tons)
      for logistics hubs 6 7 .
    2. Temperature Requirements:
      Quick-freezing (-40°C), ice-temperature (-1-0°C),
      or CA storage (0z ≤5%) .
    3. Energy Standards:
      Prioritize IPLV≥4.2 systems with heat recovery
      to reduce energy use
  • FCU (Fan Coil Unit)

    FCU (Fan Coil Unit)

    FCU (Fan Coil Unit)

    Description

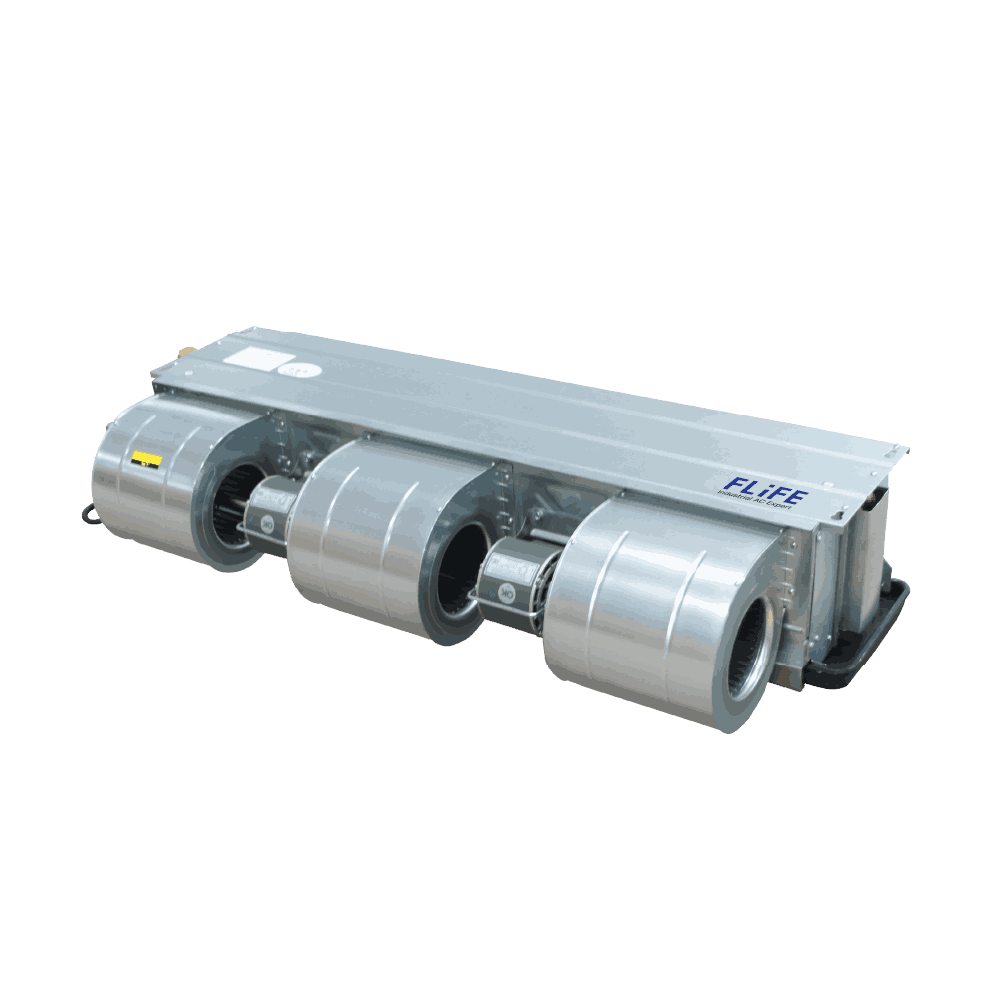
    FLIFE Fan Coil Unit (FCU)

    Core Advantages:

    • Core Structure & Working Principle
    • ​Components: Consists of a fan, heat exchange coil (copper tubes with aluminum fins), water piping, casing, condensate tray, and air filter.
    • ​Types:
    • ​By static pressure: Standard (low static pressure) vs. high static pressure.
    • ​By coil rows: Two-row (standard cooling) or three-row (high cooling capacity).
    • ​By piping: Dual-pipe (shared cooling/heating), three-pipe (separate cooling/heating loops), or four-pipe (fully independent cooling/heating)
    • ​Operation: Forces indoor air circulation via a fan, exchanging heat with chilled/hot water from a central system. Chilled water (7–12°C) or hot water (40–50°C) is supplied externally, with fresh air introduced via a separate ventilation system

    Technical Advantages:

    • ​Flexibility: Adjustable fan speeds and dynamic cooling capacity for zoned temperature control.
    • ​Energy Efficiency: Eliminates large ducts, reducing energy consumption by 20–30% compared to full-air systems.
    • ​Compact Design: Available in horizontal, vertical, or cassette configurations, ideal for space-constrained areas like hotel rooms and offices
  • Water-Cooled Chiller Screw

    Water-Cooled Chiller Screw

    Water-Cooled Chiller Screw

    Return air type/Fresh air type

    Description

    FLIFE High Static Pressure Ducted Unit delivers exceptional performance for industrial and commercial air management needs.

    Core Advantages:

    • ​Powerful Static Pressure, Stable Airflow: With an ESP (External Static Pressure) of up to ​400Pa, it effortlessly tackles long ductwork or complex ventilation systems, ensuring uniform airflow coverage across large spaces and eliminating weak airflow at terminal points.
    • ​Customizable Cooling & Airflow: Offers a wide range of cooling capacity and airflow options, tailored to spaces of all sizes—from compact zones to expansive areas exceeding 10,000㎡—meeting diverse temperature control and ventilation demands.
    • ​Industrial-Grade Reliability: Engineered for harsh environments, it features corrosion-resistant materials and precision manufacturing. Built to withstand factory challenges like high temperatures and dust, it operates flawlessly 24/7 with minimal downtime and extended longevity.
    • ​Energy Efficiency & Sustainability: Equipped with high-efficiency inverter compressors and smart controls, it reduces energy consumption by ​over 30% compared to conventional models. Paired with eco-friendly refrigerants, it balances performance with environmental responsibility, helping businesses achieve carbon reduction goals.

    Versatile Applications:

    • ​Factories & Workshops: Rapidly adjusts temperature and humidity to safeguard equipment stability and worker comfort.
    • ​Healthcare Facilities: Delivers clean airflow and precise temperature control for operating rooms, wards, and other critical areas.
    • ​Commercial Spaces: Quiet, high-volume airflow creates a comfortable environment in malls, exhibition halls, and open-plan venues, enhancing customer experience.
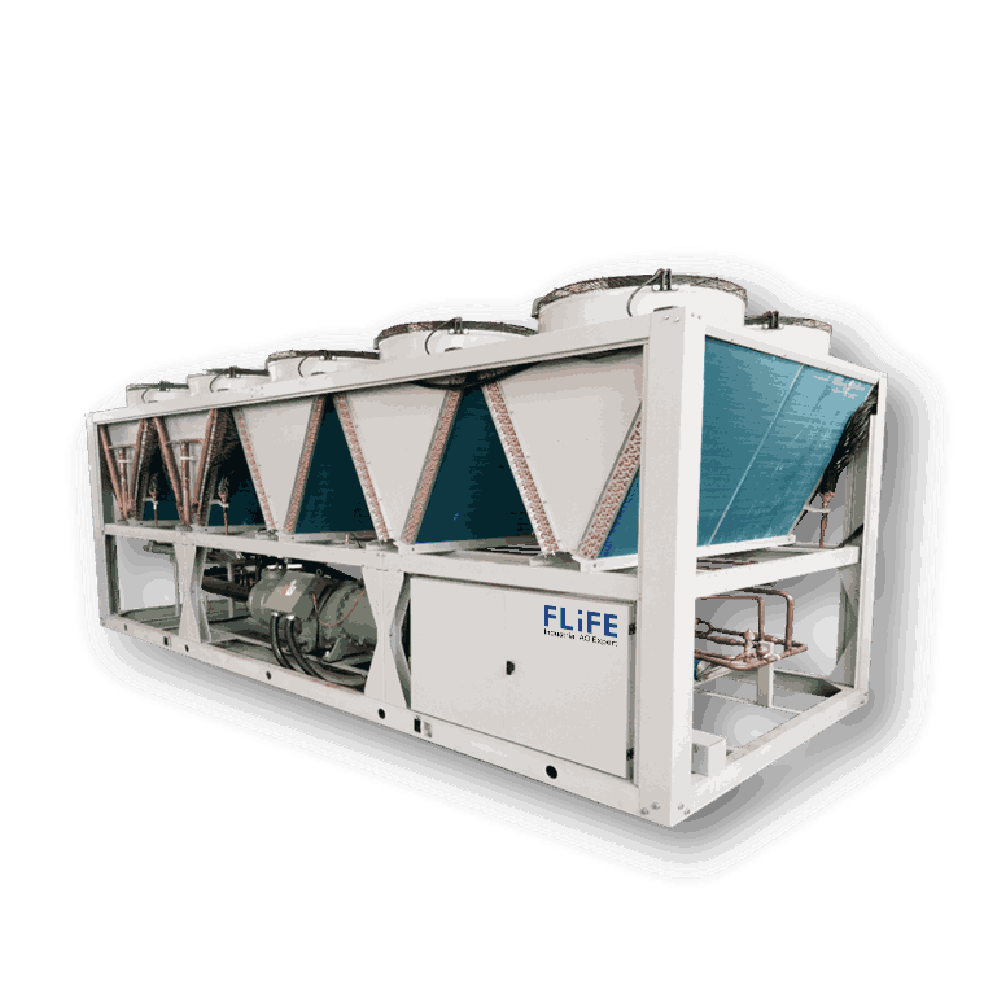
  • Air Cooled Chiller Screw

    Air Cooled Chiller Screw

    Air Cooled Chiller Screw

    Inverter/Non-Inverter

    INVERTER :372-1530kW

    NON-INVERTER : 400-815kW

    Product Features

    • ESP has a wide selection range, up to 400pa
    • A wide selection range of cooling capacity and air volume to meet a variety of usage scenarios – Customizable filters to meet scene cleanliness requirements

    Description

    FLIFE Air-cooled screw chillers excel in ​energy efficiency, ​adaptability, and ​low maintenance, making them ideal for commercial, industrial, and critical applications.
    Core Advantages:

    1. ​High Efficiency & Energy Savings:
    • Variable frequency technology allows 10%–100% load adjustment, improving partial-load efficiency by 20%–30%
    • Uses eco-friendly refrigerants (R134a/R407C) and heat recovery systems to reduce carbon emissions
      ​2. Easy Installation & Maintenance:
    • No cooling towers or dedicated room required, suitable for outdoor installation
    • Modular design supports split configurations (indoor/outdoor units) for hot climates
    1. ​Durability & Adaptability:
    • Corrosion-resistant frames and EPDM seals ensure stable operation in high-humidity or salt-spray environments
    • Operates in extreme temperatures (-18°C to 43°C), suitable for year-round cooling and ice storage systems

    Versatile Applications:

    • Commercial Buildings
    • Food Processing
    • Pharmaceuticals
    • Industrial Manufacturing

  • Air-Cooled Chiller Module

    Air-Cooled Chiller Module

    Air-Cooled Chiller Module

    Description

    Air-cooled modular units excel in ​flexibility, ​energy efficiency, and ​durability, making them ideal for dynamic environments.

    Core Advantages:

    1. ​Flexible Scalability
Modular design allows units to expand by adding/removing modules based on load requirements, avoiding energy waste from oversizing
    2. ​High Energy Efficiency
    • ​IPLV ≥5.0: Optimized partial-load efficiency with multi-module coordination
    • ​Smart Controls: AI-driven load prediction and adaptive operation reduce energy consumption by 15–20%
      ​3. Reliability & Redundancy
    • Fault-tolerant operation: If one module fails, others continue running
    • Easy maintenance: Individual modules can be repaired without system shutdown
    1. ​Space-Saving & Easy Installation
    • Compact structure fits rooftops or tight spaces
    • No cooling towers or complex piping required
    1. ​Year-Round Versatility
Supports ​cooling + heating modes (heat pump models) and operates in extreme temperatures (-35°C to 43°C)

  • Water-Cooled Cabinet AC Unit

    Water-Cooled Cabinet AC Unit

    Water-Cooled Cabinet AC Unit

    Cooling Only / Constant Temperature and Humidity

    Description

    FLIFE Water-cooled Cabinet AC Unit – – Versatile Climate Control for Demanding
    Environments!
    Core Advantages:

    • Dual Product Types
Choose between ​Cooling-Only and ​Constant Temperature & Humidity models:
    • ​Cooling-Only: Rapid cooling for offices, retail spaces, and general temperature control.
      ​- Constant T&H: Precision temperature (±3°C) and humidity (±5% RH) management, ideal for labs, data centers, and pharmaceutical environments.
    • 3D Airflow Flexibility
Three installation-ready airflow configurations:
    • ​Front Return & Front Supply (FRFS): Direct airflow for open areas requiring fast cooling.
      ​- Front Return & Top Supply with Duct (FRTS-D): Concealed ceiling distribution via ducts, perfect for high-ceiling spaces like airports.
    • ​Rear Return & Top Supply with Duct (RRTS-D): Space-saving rear intake + top ducted supply, optimized for mechanical rooms or compact layouts.
    • Industrial Durability & Effortless Installation
    • ​Robust Construction: Monolithic casing with 304 stainless steel框架 resists vibration, corrosion, and harsh factory conditions.
    • ​Multi-Mounting: Ceiling suspension, floor-standing, or wall-adjacent installation. Pre-installed dampers and anti-vibration pads reduce maintenance efforts by 30%.
      Versatile Applications:
    • Industrial Facilities: Precise temperature and humidity control in factories and warehouses protects machinery and inventory.
    • ​Transportation Hubs: Efficient cooling in high-traffic areas like airports and stations enhances passenger comfort.
    • ​Commercial Spaces: Maintain consistent comfort in offices, meeting rooms, and more.